

News Detail
Welding Table Accessories: Building a Complete Modular Fixturing System
author:hxrtools Time:2026-10-26 18:58:43 Click:104
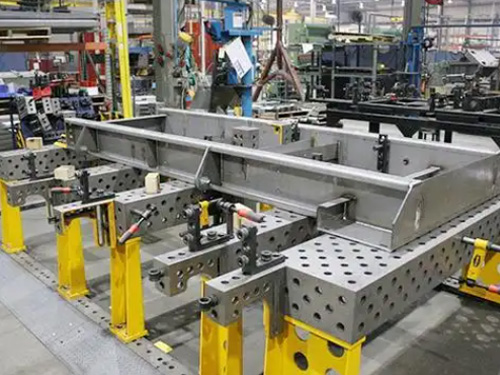
Buying a 3D welding platform and stopping there is the most common — and most expensive — mistake in flexible fixturing. The table is the coordinate system; the welding table accessories are what actually hold the part. Shops that budget properly for clamps, stops and locating modules get the promised setup-time reduction. Shops that buy the plate and a handful of clamps end up with an expensive flat surface and the same old fabrication problems.
The Core Accessory Families
| Accessory | Function | Where It Earns Its Keep |
|---|---|---|
| Quick clamps | Fast, lever-actuated holding force | Repetitive manual welding stations |
| Locating pins / stop pins | Define the part's X-Y datum in the bore grid | Every setup — the true accuracy carrier |
| Angle brackets | Create vertical and inclined clamping faces | Out-of-position and 3D frame welding |
| V-blocks | Locate round tube, pipe and shaft | Pipework, handrails, chassis tubes |
| Support blocks / risers | Elevate and level irregular workpieces | Castings, weldments with uneven datum faces |
| C-type clamps | General-purpose heavy clamping | Thick plate fit-up and tacking |
How Many Accessories Do You Actually Need?
A working rule for a two-operator station: enough modules to build two complete fixtures simultaneously — one in use, one being assembled for the next job. In practice that means roughly:
8–12 locating/stop pins per square metre of table
6–10 quick clamps per operator
4–6 angle brackets for vertical work
2–4 V-blocks if tube or pipe is welded
A set of support blocks and spacers in graded heights
Matching Accessories to the Hole System
Accessories must match the grid: D28 modules for Ø28 mm bores on a 100 mm pitch, D16 modules for Ø16 mm bores on a 50 mm pitch. Confirm both the bore diameter and the shank standard before ordering — "looks similar" is not compatibility, and a loose-fitting shank reintroduces exactly the positioning error the system was bought to eliminate.
Material and Finish Considerations
Body: hardened alloy steel or cast iron, machined to mate precisely with the bore.
Finish: blackened, galvanized or nitrided to survive spatter and shop humidity.
Wear parts: pins and clamp pads should be treated as consumables and replaced before they become sloppy.
Table surface: nitrided to HV 450–630, so accessories seat cleanly and do not gall the bore.
Maintaining the Accessory System
Keep bores free of spatter — use a reamer or bore brush, never a grinder.
Store modules on a rack, not loose in a drawer where contact faces get damaged.
Apply light anti-rust oil to steel modules during humid seasons or shutdowns.
Re-check that pins seat without rocking; a worn pin silently downgrades the whole table's accuracy.
FAQ
Q1: Are your accessories interchangeable with other brands?
Both D28 and D16 follow universal industry-standard dimensions, so our modules work with mainstream tooling sets — no proprietary lock-in.
Q2: Can I buy the table first and add accessories later?
Yes, but budget for the full kit at purchase. Partial kits are the main reason shops fail to achieve the expected changeover savings.
Q3: Do you offer custom fixtures?
Custom locating and clamping modules can be designed and machined for unusual workpieces; send drawings for evaluation.
Spec Your Table and Kit Together
Hebei Haoxinran Machinery Manufacturing Co., Ltd (HXR Tools) supplies calibrated 3D welding platforms together with matched D28/D16 clamps, pins, brackets, V-blocks and support blocks. Send your part drawings and we will propose a complete fixture kit sized to your station. Request a kit proposal.
 HOT PRODUCTS

 CONTACT US
—— E-mail:project@haoranmj.com
—— Whatsapp:+86 18932785670
—— Tel:+86 18932785670
—— Add:Across from Sanjing Distillery on Road 4, Botou Economic Development Zone, Cangzhou City, Hebei Province