

News Detail
3D 5-Axis Laser Cutting Processing for Automotive Moulds and Structural Parts
author:hxrtools Time:2026-11-06 20:09:30 Click:174
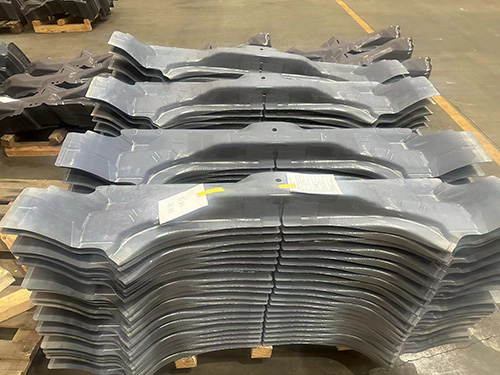
Flat-sheet laser cutting is a solved problem. The parts that still create bottlenecks are the three-dimensional ones — a moulded automotive panel needing its flash trimmed, a hot-formed pillar with holes on three different planes, a tube structure with compound-angle ends. 3D 5-axis laser cutting solves these in a single clamping by keeping the beam normal to a continuously moving surface, eliminating the re-fixturing, manual trimming and hard tooling that conventional methods require.
What 5-Axis Adds Over 3-Axis Cutting
Normal incidence on curved surfaces: the head tilts to keep the beam perpendicular, so cut quality stays consistent over the whole contour.
Single-setup completion: trimming, piercing and edge profiling on multiple planes without re-clamping — no cumulative fixture error.
No hard trimming die: ideal for prototypes, engineering changes and low-to-mid volumes where a die cannot be justified.
Non-contact processing: no tool pressure, no part distortion, minimal burr on thin materials.
Typical Applications
| Industry | Parts processed |
|---|---|
| Automotive & mould | Instrument panels, door inner panels, pillar trims, bumper openings, moulded part flash trimming |
| Hot-formed components | A-pillar / B-pillar reinforcements, door beams, ultra-high-strength safety parts |
| Structural fabrication | Tube ends, square-tube notching, gusset and bracket profiles |
| Machinery & enclosures | Cabinet cut-outs, formed covers, equipment housings |
| Prototyping | One-off development parts before hard tooling commitment |
Automotive Mould: Where Tolerances Are Won or Lost
An automobile mould programme lives or dies on repeatability. A trimming operation that varies by a few tenths of a millimetre changes how the panel fits the body-in-white fixture — and that shows up downstream as assembly rework. Two factors dominate the result:
Fixture datum quality: the part must be held repeatably. Shops that pair 3D laser cutting with a calibrated 3D welding platform or dedicated fixture base get measurably tighter distributions than those using improvised supports.
Verified geometry: formed parts spring back. Scanning the actual part and cutting against measured geometry, instead of nominal CAD, is what keeps first-piece accuracy high.
Preparing Parts for 3D Laser Processing
Supply 3D CAD (STEP / IGES) plus, where possible, scanned geometry of the actual formed part.
Define the trim line clearly and mark allowable tolerance zones.
State material and thickness — these set cutting speed, assist gas and edge quality expectations.
Identify clamping surfaces that will not be cut, so the fixture design can use them.
Confirm batch size: prototype, pilot or series, since this changes fixture strategy.
Quality Assurance We Apply
Every project is verified, not assumed. Our facility runs a Swedish-imported 3D coordinate detector for dimensional verification and a Swedish blue-ray scanner for free-form surface comparison against CAD — the same metrology chain used for our welding platforms and cast iron platforms. This closes the loop between cutting and inspection and lets us report actual deviation rather than nominal intent.
Why Combine Laser Processing With an In-House Foundry and Machining Shop
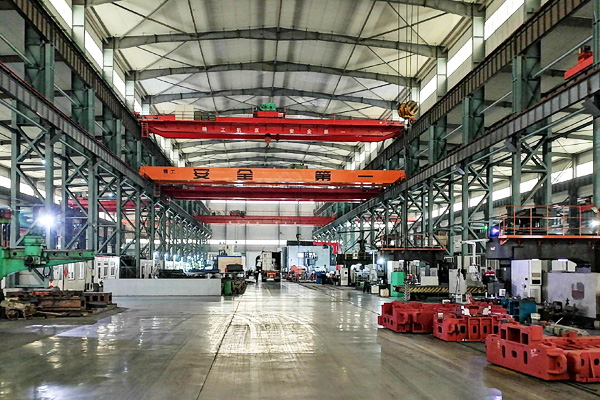
Trimmed parts rarely exist in isolation — they become weldments, assembled structures or production fixtures. Having casting, machining, heat treatment, precision plate manufacturing and 5-axis laser capability under one roof removes the hand-off delays and tolerance stack-ups that appear when each step is outsourced to a different vendor.
FAQ
Q1: Can you cut hot-formed ultra-high-strength steel?
Yes — 5-axis laser is one of the few practical methods for trimming hardened hot-formed parts without mechanical tooling.
Q2: Do I need to supply a fixture?
No. We can design and build the fixture, and where appropriate base it on our modular D28/D16 platform system for future reuse.
Q3: What volumes make economic sense?
Prototypes through mid-volume series. Above high-volume thresholds, a dedicated trimming die may still be cheaper per piece — we will advise honestly.
Send a 3D Model for Processing Evaluation
Hebei Haoxinran Machinery Manufacturing Co., Ltd (HXR Tools) — established 2009, 90-acre Botou facility, 40+ CNC machines, Swedish CMM and blue-ray scanning, Norwegian high-frequency quenching, CE-verified to EN ISO 12100:2010. Upload your STEP file and required tolerance for a processing proposal covering 3D 5-axis laser cutting, automobile mould work and fixture design. Request a processing quote.
 HOT PRODUCTS

 CONTACT US
—— E-mail:project@haoranmj.com
—— Whatsapp:+86 18932785670
—— Tel:+86 18932785670
—— Add:Across from Sanjing Distillery on Road 4, Botou Economic Development Zone, Cangzhou City, Hebei Province